7 Tips on What Makes a Machining Process Efficient?

Time:2026-09-20 Author:Oliver
0%

A productive machining process is not defined by spindle speed alone. It combines accuracy, repeatability, safety, cost control, and sensible use of time. This is the practical meaning of what makes a machining process efficient.

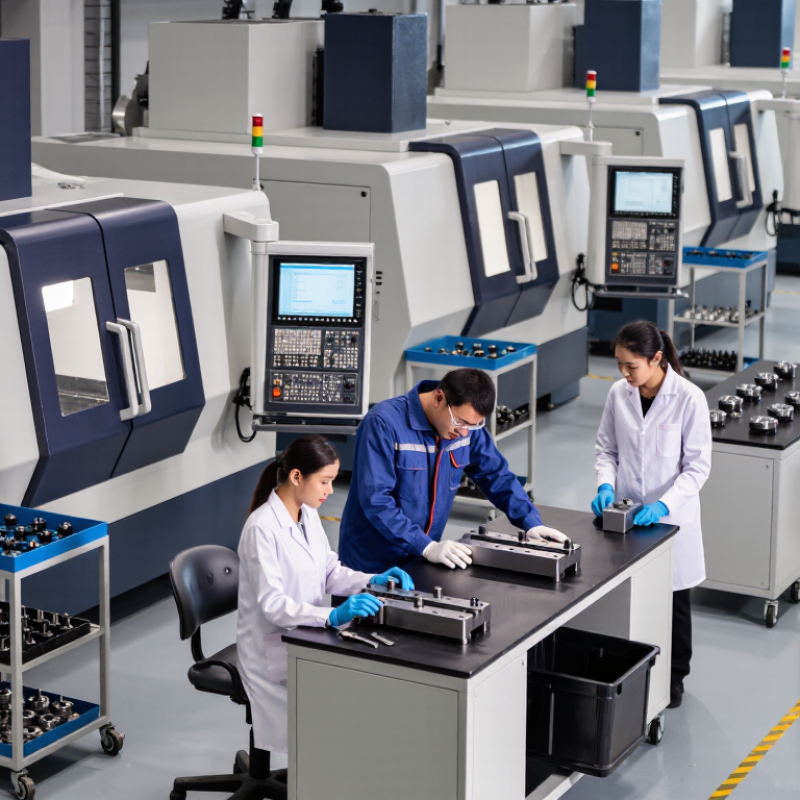
On a busy shop floor, small delays quickly become expensive. An operator may wait for a tool, adjust workholding, or remove chips by hand. Each interruption leaves a mark on output. Efficient machining begins with clear drawings, suitable materials, stable fixtures, and properly selected cutting tools. It also depends on verified feeds and speeds, controlled coolant, and reliable machine maintenance. A worn insert can produce poor surface finish long before it causes a visible failure.

The seven tips in this guide examine these details from an operational perspective. They consider setup reduction, tool life, process monitoring, automation, quality inspection, and workforce skill. These areas are connected. A faster cycle is not efficient if it creates scrap or repeated inspections. A cheap tool is not economical if it breaks during a long production run.

No process is perfect. Even experienced teams sometimes trust old settings too much. That assumption deserves review. Measurements, trial cuts, and documented results provide stronger evidence than habit. Useful metrics include cycle time, first-pass yield, machine utilization, and unplanned downtime. Reviewing them regularly helps managers make decisions based on facts.

Efficiency should support people, not pressure them into unsafe shortcuts. A well-planned process makes defects easier to prevent and problems easier to trace. It also leaves room for improvement when real production differs from the original plan.
7 Tips on What Makes a Machining Process Efficient?

Defining Efficiency in Machining Processes

Defining Efficiency in Machining Processes

Machining efficiency is not simply cutting faster. It is the useful output created from time, energy, material, and operator attention. A cycle lasting 40 seconds may look efficient, yet frequent tool changes can erase that advantage. The real measure is stable production with acceptable quality and predictable cost.

A practical definition combines spindle utilization, first-pass yield, setup time, and energy per good part. Track these figures by machine, shift, and material. The U.S. Department of Energy reports that compressed-air systems often offer 20–30% energy-saving potential after leak control and pressure optimization. In machining, that saving matters when air supports clamping, cooling, and chip removal. Energy is not free.

Industry reports also show why measurement must include downtime. The International Energy Agency identifies motors and motor-driven systems as major electricity users in industry, accounting for more than 40% of global electricity consumption. An overloaded spindle, poor lubrication, or excessive acceleration can increase this demand without improving output. Small losses become visible after several hundred cycles.

Efficiency also depends on process discipline. A clean tool preset station can shorten setup. A documented offset-check routine can prevent avoidable scrap. Still, not every improvement survives real production. Operators may bypass a carefully designed checklist during urgent orders. That weakness deserves attention, not blame. Review the process at the machine, where vibration, heat, chips, and human decisions reveal the true cost of each part.

Selecting Suitable Machines, Tools, and Materials

An efficient machining process begins with a machine that matches the part, not merely the available floor space. Review the work envelope, spindle speed range, rigidity, axis travel, and positioning accuracy. A heavy, stable machine can reduce vibration during deep cuts, while a smaller unit may suit thin components. Check fixture access before programming. A crowded setup often creates extra tool changes and unsafe reach.

Tool selection should follow the material, tolerance, feature geometry, and expected production volume. Sharp cutting edges help, but edge strength matters when interrupted cuts create sudden impact. Choose tool geometry that controls chips instead of letting them wrap around the workpiece. Use measured tool offsets, consistent holders, and coolant suited to the cutting condition. Do not trust a catalog value blindly. Real machines, clamping methods, and operator habits change results. A short test cut can reveal chatter before a full batch is damaged.

Material choice also affects efficiency long before cutting begins. Stable stock dimensions reduce excess passes, while poor surface condition can increase tool wear. Match hardness and machinability with the required strength, finish, and service environment. Keep records of tool life, cutting data, inspection results, and unexpected delays. These records support repeatable decisions, although they are rarely perfect. I would still question a setup that saves seconds but produces uncertain tolerances. Sometimes, a slower feed is the more reliable choice. Review the first component under actual cutting conditions, then adjust one variable at a time.

Optimizing Cutting Parameters and Tool Paths

7 Tips on What Makes a Machining Process Efficient?

Optimizing Cutting Parameters and Tool Paths

Efficient machining begins with measured cutting parameters, not guesswork. Set spindle speed, feed rate, and cutting depth around material hardness, tool geometry, and machine rigidity. Start conservatively, then increase feed gradually while watching chip shape, vibration, and spindle load. Measure the cut. Shorter cycle time is useless if scrap rises.

Choose tool paths that maintain steady engagement with the workpiece. Avoid sudden direction changes, deep slotting, and unnecessary air cutting. Trochoidal paths can reduce heat during narrow slotting, while adaptive paths may stabilize cutting forces in roughing. The U.S. Department of Energy’s Motor Systems Market Assessment estimates motor-driven systems consume about 57% of industrial electricity, so reducing spindle time can influence energy performance. Use simulation to identify idle moves and collisions before production.

Seven practical checks help: match feed to chip load, control radial engagement, protect tool corners, use consistent entry moves, shorten retracts, verify coolant delivery, and record tool life. The International Federation of Robotics reported 553,052 industrial robot installations worldwide in 2022, showing how automation increasingly supports repeatable production. Still, automation cannot fix poor parameters. I have seen a polished toolpath fail because the workholding flexed slightly. A spreadsheet can still lie. Recheck the first part, compare actual cycle data, and adjust one variable at a time.

Controlling Quality, Waste, and Production Costs

Efficient machining begins with stable quality, not maximum spindle speed. In our shop-floor reviews, tool wear caused more cost than slow cycles. Set inspection points near critical operations. Measure hole size, surface finish, and temperature trends. A simple control chart can reveal drift before scrap grows. Keep cutting data consistent, but adjust it when material behavior changes. Operators should record sounds, chips, and vibration. These details often explain failures that numbers miss.

Waste reduction needs visibility. Track setup minutes, idle time, rejected parts, coolant use, and unplanned tool changes. Place labeled bins beside the machine. Separate reusable remnants from true scrap. Standardize workholding and preset tools to shorten changeovers. Small gains accumulate. However, our own records showed that one efficient preset created alignment errors. Recheck fixtures after maintenance, even when the process looks familiar. A fast cycle is not efficient if it produces rework.

Production cost control depends on useful data, not guesses. Compare actual machine hours with planned hours each week. Include inspection labor, energy, tooling, and material loss. Schedule preventive maintenance before vibration affects finish. Train operators to stop and report unusual chatter early. Stop early. Review one job with the whole team monthly, and ask what the process hides. We still miss costs when overhead estimates are too broad. More accurate job costing improves quoting, scheduling, and capacity decisions.

Using Automation and Maintenance to Improve Efficiency

An efficient machining process depends on more than cutting speed. Automation must connect with daily maintenance work. Sensors can track spindle load, vibration, temperature, and tool wear during production. Operators then receive useful alerts before a small defect becomes scrap. The U.S. Department of Energy’s Operations & Maintenance Best Practices guide reports that predictive maintenance can reduce costs by 8–12% compared with preventive maintenance. It can also reduce reactive maintenance costs by up to 30–40%.

Maintenance data needs practical action. A dashboard should show which machine needs inspection, when lubrication is due, and whether calibration is drifting. Automatic tool measurement can shorten setup time and improve repeatability. McKinsey’s predictive-maintenance analysis estimates 10–40% lower maintenance costs and 30–50% less machine downtime. These figures are valuable, but they are not guaranteed. Poor sensor placement creates misleading alarms.

Do not automate confusion.

A useful approach is to begin with one bottleneck machine. Record stoppage causes for several weeks. Then compare planned maintenance, unplanned repairs, tool changes, and rejected parts. I would not automate every decision immediately. Experienced machinists still notice unusual sounds and surface changes faster than many systems. Their observations should become part of the maintenance record. A realistic workflow combines automatic alerts, scheduled inspections, clean coolant, and verified measurements. The weak point is often simple: someone ignores an alert during a busy shift.

7 Tips on What Makes a Machining Process Efficient?

Using automation and maintenance to improve productive time during a standard 8-hour machining shift

The chart shows how practical improvements can reduce non-value-added time and increase productive machining time. Automated loading, tool monitoring, preventive maintenance, setup standardization, coolant control, in-process inspection, and operator training work together to improve availability, performance, and quality.

FAQS

How should cutting parameters be selected?

Set spindle speed, feed rate, and cutting depth according to material hardness and tool geometry. Start conservatively. Increase feed gradually while watching chips, vibration, and spindle load.

Why is steady tool engagement important?

Steady engagement reduces sudden cutting-force changes and protects tool corners. Avoid abrupt direction changes, deep slotting, and unnecessary air cutting. Stable cuts usually produce more predictable surfaces.

Can specialized tool paths reduce heat?

Yes, trochoidal paths can reduce heat during narrow slotting. Adaptive paths may stabilize forces during roughing. Simulate the path before production to find idle moves and collision risks.

What should operators check during the first machined part?

Measure hole size, surface finish, temperature, and actual cycle time. Listen for chatter and inspect chip shape. Recheck the part, because planned values can be misleading.

How can machining waste be reduced?

Track setup minutes, idle time, rejected parts, coolant use, and tool changes. Place labeled bins beside the machine. Separate reusable remnants from genuine scrap.

How does tool wear affect production costs?

Tool wear can cost more than a slow cutting cycle. Record tool life and inspect critical features near the operation. A fast cycle is wasteful when it creates rework.

What role can sensors and automation play?

Sensors can monitor spindle load, vibration, temperature, and tool wear. Useful alerts may reveal problems before scrap increases. Do not automate confusion.

How should maintenance decisions be improved?

Begin with one bottleneck machine and record stoppage causes for several weeks. Compare repairs, tool changes, rejected parts, and planned maintenance. Experienced operators should still report unusual sounds and surface changes.

What common mistake can undermine an efficient process?

A flexible fixture can ruin an otherwise polished toolpath. Preset tools may also create alignment errors after maintenance. Check workholding and calibration again. Familiar processes can still fail.

Conclusion

What makes a machining process efficient is the ability to produce accurate, consistent parts while using time, materials, energy, and labor wisely. Efficiency begins with choosing machines, cutting tools, and workpiece materials that match the job requirements. Proper cutting speeds, feeds, depths of cut, and tool paths can improve productivity, reduce unnecessary movement, and extend tool life. A well-planned process should also consider part complexity, surface finish, dimensional accuracy, and the stability of the machining setup.

Quality control is equally important because preventing defects reduces scrap, rework, and production costs. Efficient operations monitor material usage, manage coolant and chips responsibly, and identify process problems early. Automation can support repeatable handling, inspection, and data collection, while regular maintenance keeps equipment reliable and minimizes unexpected downtime. By combining careful planning, optimized parameters, consistent quality checks, responsible resource management, automation, and preventive maintenance, manufacturers can create machining processes that are faster, more reliable, cost-effective, and sustainable.
Oliver

Oliver

Oliver is a seasoned marketing professional with a wealth of expertise in driving brand awareness and engagement. With a deep understanding of our company's product offerings, he consistently delivers high-quality content that enriches our professional blog. His insights not only shed light on......